
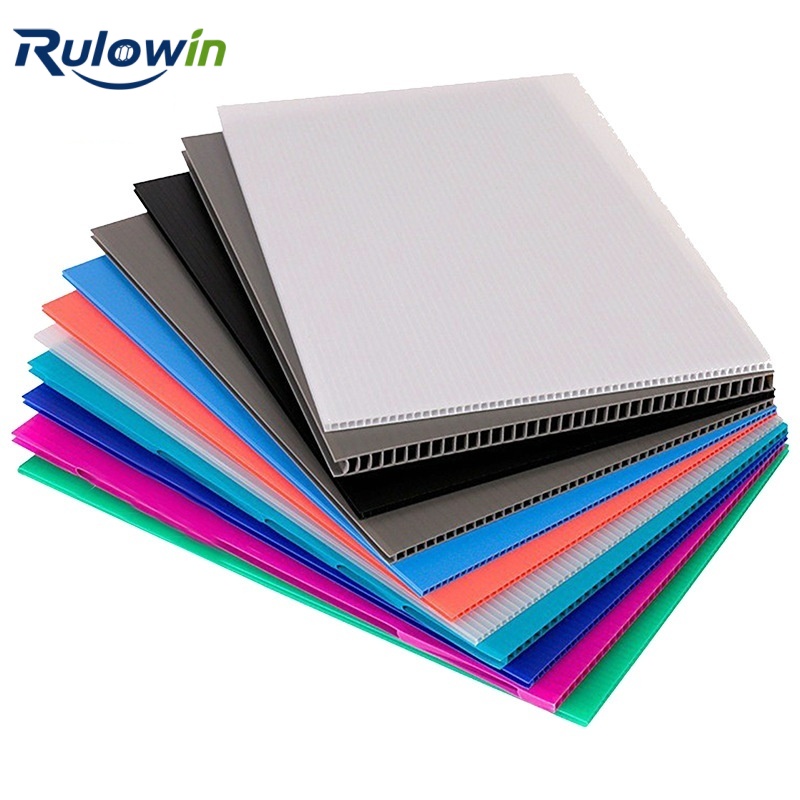
Corrugated PP sheet is not isotropic. The internal flutes run in one direction, and the sheet is dramatically stiffer and stronger along them than across them. This is not a minor effect, and it is the single most common reason a sheet performs differently than expected.
Why it behaves that way
The flutes are vertical walls connecting the two skins. Loaded along the flutes, those walls act like the web of an I-beam and resist bending well. Loaded across them, the walls can lean and buckle, and the sheet folds comparatively easily.
The practical consequence is that the same sheet can hold a load along one axis and sag visibly along the other.
Where it helps you
Folding. The sheet hinges cleanly across the flutes – that is, with the fold line running along the flute direction – and resists folding in the other direction. Every corrugated box relies on this: the score lines are placed across the flutes so the box folds where you want and stays rigid where you need it.
Where it hurts you
- A shelf or a base loaded across the flutes will sag where the same sheet along the flutes would hold.
- A vertical panel with the flutes running horizontally will bow outward under its own weight and any load.
- A box wall with flutes running horizontally has almost no stacking strength. Box flutes should run vertically.
- Cut-outs and holes that interrupt the flutes remove far more strength than the same hole placed between them.
How to tell which way the flutes run
Look at a cut edge. On an unsealed edge you can see the channels directly. On a sealed edge, flex the sheet – it bends easily one way and resists the other, and the easy direction is across the flutes. If you are specifying, state the flute direction relative to a dimension on the drawing rather than leaving it to convention.
Specifying it properly
Write it down. “Flutes parallel to the 1200 mm dimension” is unambiguous; “flutes vertical” is not, unless everyone agrees which way up the panel goes. If the sheet is being cut into blanks, specify the flute direction on the blank, because that is what matters in use.
Working around it
Sometimes you cannot orient the flutes usefully – a square base needs stiffness in both directions. Options:
- Cross-laminate two sheets with the flutes at right angles
- Add a frame or a rim that carries the load in the weak direction
- Use a honeycomb panel instead, which behaves the same in both directions
- Increase thickness in the weak direction, which is the least efficient fix but sometimes the simplest
How it affects cutting and waste
Flute direction also determines how efficiently blanks come off a sheet. Because the flutes should run the same way in every blank, the layout is constrained, and a poorly chosen blank orientation can add noticeable waste.
This is worth checking at the quotation stage, because it is invisible in the unit price. Two suppliers quoting the same sheet price can differ meaningfully in cost per usable blank once the nesting is worked out.
If your volumes justify it, it is worth having the sheet produced with the flutes running the way your blank layout wants rather than the way the extruder finds convenient. It is a manufacturing option rather than a fixed constraint, and it is rarely offered unless asked for.
What we can do
We supply corrugated sheet cut with the flute direction controlled, and we will ask which way you need it before quoting. If you tell us how the panel is loaded, we can usually say whether flute orientation alone solves your problem or whether you need one of the workarounds above.