
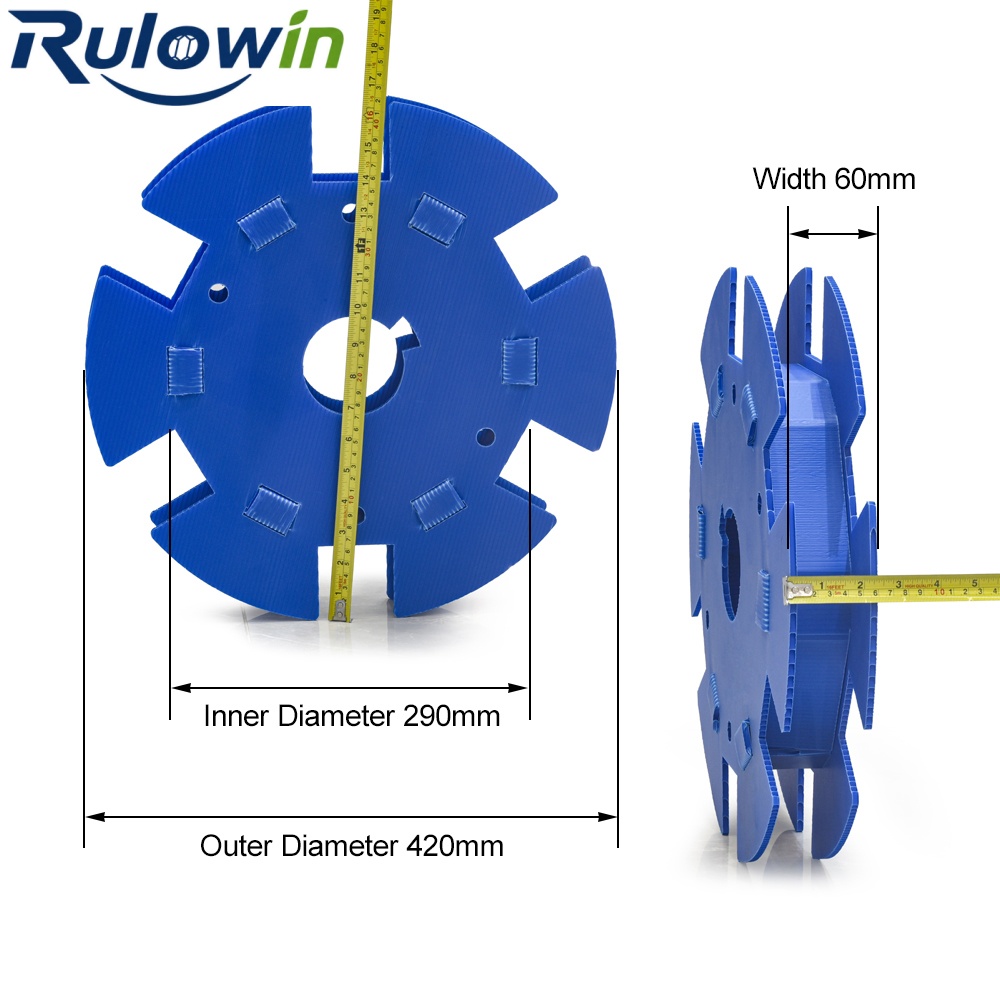
Rubber extrusion — seals, gaskets, profiles, weatherstrip — comes off the line soft and gets softer to handle as it ages. Every rule for spooling it follows from one property: it takes a permanent set from very little encouragement.
The central problem
Press a rubber profile against anything with moderate pressure and leave it long enough, and it stays pressed. Leave it wound under tension and it takes a set at the bend. Both effects are permanent, and both get worse with:
- Time. The dominant variable, which we discussed generally in our piece on long-term wound storage.
- Temperature. Everything gets faster warm.
- Pressure. Including pressure from its own layers.
Keep packs shallow
The single most effective thing is fewer layers. Each layer adds to the pressure on the ones beneath, and the innermost deals with the accumulated weight of everything above it.
In practice this means larger flanges and smaller fill depth than people instinctively choose — which runs directly against the general guidance about using available space. For elastomer it is usually the correct trade.
Keep tension low
Lower than feels right. Rubber profile does not need tension to wind well; it needs enough to lay consistently and not much more. Higher tension means stretched product, which means it either recovers at indeterminate length or does not recover at all.
Stretching is a particular trap because the product may be specified by length. Wind a stretched profile and you have effectively sold the customer less than they thought they bought.
Large core
Lower curvature at the base of the pack reduces both set and compression there. This replicates what every soft-product article in this series recommends — see the parallel discussion for soft wire — and it costs packaging efficiency for the same reason.
Flatness matters more than roundness
A profile keeps whatever cross-section it is held in. Press it at a contact line and it flattens there permanently. This means:
- Core surface must be smooth and have no seams or ridges standing proud
- Nothing on the flange face can contact product
- Support needs to be broad, not line contact
Talc and dusting
Some rubber profiles are dusted to prevent blocking. The dust gets everywhere, including into the bore and onto subsequent products spooled on the same reel. If you are running dusted and undusted products on shared equipment, that is worth knowing.
Blocking
Some compounds will stick to themselves given time and pressure. Interlayer separation addresses it and costs handling — our article on interlayer sheets covers this. Whether it is needed depends on the compound, which is a question for whoever makes the profile.
Cleaning between products
Reusable reels carrying different compounds need cleaning, and that is where most people discover that their cleaning method damages PP rather than rubber. The specific cautions are in our cleaning article.
What we recommend
Large core, shallow fill, low tension, smooth everything, and short storage before use. In that order of importance.
Also worth considering: whether your customers need this spooled at all. Some profiles ship better coiled loose in a box, and the spool is solving a handling problem that another form of packaging handles better. We make our hollow board spools and would still rather you used whichever packaging actually works.
A note on splicing
Rubber profile runs are spliced, and every splice is a thickness variation travelling through the pack. Each one creates a localised high spot, and by twenty layers that high spot has multiplied enough to matter — the same propagation described generally in our piece on the first three layers, except that here the irregularity keeps arriving throughout the wind rather than appearing once at the start.
This argues for lower tension than you would otherwise use, and for accepting a fill level well below the flange. Nothing you do prevents splices; what you control is how much damage each one does.
Checking a reel before you return it to service
Two minutes per reel catches most problems: look for any ridge or seam standing proud on the core, check the flange faces are clean and smooth, and check the reel still runs true. Any of those three will imprint into soft product, and all three are cheap to detect once somebody is looking.
Our sealing and extrusion customers who do this routinely report noticeably fewer complaints than the ones who do not, and it costs less than the alternative.