
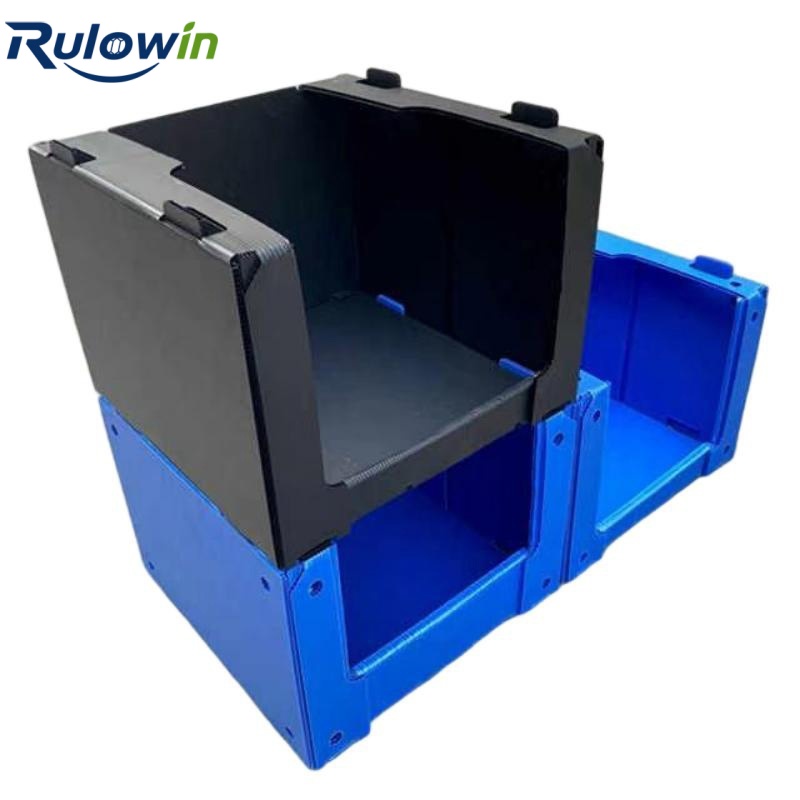
A picking wall is a system: shelf bay, divider, tote, product. When one of those four is replaced without checking the others, the result is the familiar sight of a bay with gaps at the ends, dividers that lean, and totes that have to be turned sideways to fit.
The root cause is nearly always the same. The shelf module was bought to fit the room, the boxes were bought to fit the products, and nobody checked that the first divides cleanly into the second.
The arithmetic that prevents it
Take the clear internal width of the shelf bay — not the nominal width, the measurement with the uprights and any shelf lip accounted for. Divide it by the candidate box width including its wall thickness and any divider allowance. If it does not divide to a whole number with a small margin, the bay will either be loose or over-filled.
Do the same for depth. A box that protrudes 40 mm beyond the shelf front may still work — or it may foul a door, a conveyor or a person’s knee. A box that is 60 mm too shallow wastes depth across every bay in the wall, which across a warehouse is a lot of air.
Dividers change everything
Dividers consume width. A bay that holds eight boxes with no dividers holds six with two divider rows, and the difference is invisible until the day the dividers arrive.
Two divider types behave differently:
- Full-height rigid dividers sit in grooves or slot into the shelf and are the most stable. They need the shelf or the box to have the slot pattern, so they lock you into a system.
- Box-mounted dividers — cells, partitions or inserts inside the tote — travel with the box. More flexible, and they consume internal width rather than bay width.
If your product range changes often, box-mounted wins on flexibility. If the range is stable and volumes are high, fixed bays with rigid dividers give the densest, tidiest wall.
Standardise on a footprint family
The practical answer for most operations is to pick two or three box footprints that divide cleanly into your shelf module and into each other, and then stop buying anything else. A common approach:
- A wide box for the fast movers that fills a bay
- A half-width box that takes two to the same bay
- A shallow box for depth-limited shelving
Three footprints cover most product ranges, and once they are fixed, dividers, labels, conveyor saddles and pick carts can be specified once and used everywhere. The cost of not doing this is invisible but real: every non-standard box in the wall creates a bay that is slightly less dense than it could be.
Depth deserves more thought than it gets
Picking depth is a human factors issue as much as a storage one. A deep box means reaching into it, and the second half of the depth is where mispicks concentrate — the picker grabs what is nearest rather than what is next.
Shallow, wide boxes with more forward-facing product beat deep boxes for pick accuracy, at the cost of more replenishment. For slow movers, depth is fine. For fast movers, shallow and forward-facing usually wins on pick rate alone.
Practical checklist before ordering
- Measure the clear bay, not the nominal shelf size
- Divide and confirm whole units per bay in both orientations
- Decide divider type first, then subtract its allowance from the box width
- Check the box front against doors, conveyors and rack lips
- Put one of each candidate on the actual shelf, with actual product, before ordering a container of them
Corrugated PP has an advantage here that is easy to exploit: it die-cuts to any footprint without expensive tooling, so matching a box to an awkward bay is a cheap exercise rather than a moulding project. If you send your shelf module dimensions, we can suggest two or three footprints that will tile them cleanly.