
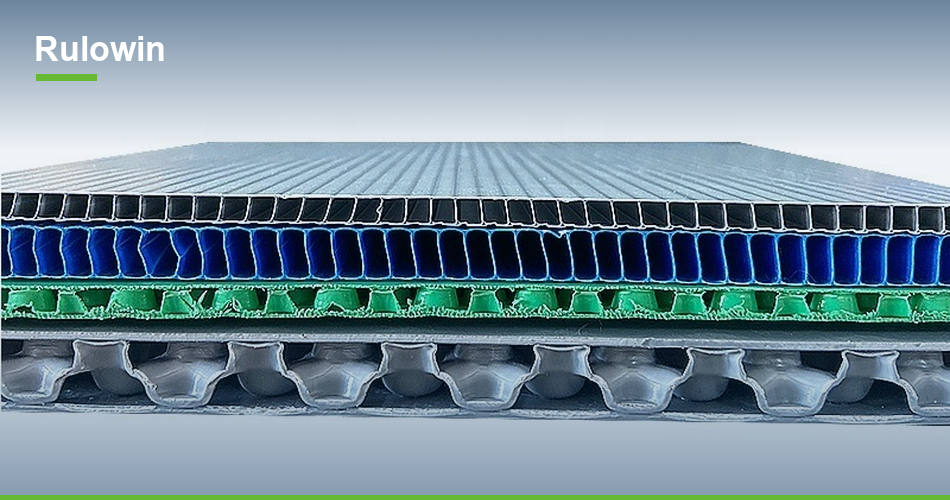
A blank that comes off the die looking perfect and refuses to fold into a square box a week later is a familiar frustration. The board has not changed — it has relaxed. Polypropylene corrugated sheet has more memory than paperboard, and a creasing operation that would be fine on fibre needs a different set of numbers on plastic.
What a crease on plastic actually is
On paperboard, a crease crushes the fibre and creates a living hinge. On corrugated PP there are two options, and they behave differently:
- Crease (emboss) without cutting. The flute is compressed between two rules. Works well on thin sheet with fine flutes; on thicker sheet the flutes resist and the crease springs back over days.
- Partial cut-through. One skin is cut, the other is left intact to act as the hinge. Sharper, more permanent folds, and the usual choice for thicker material.
The spring-back problem is worse than on fibre because PP is a polymer: it wants to return to the shape it was extruded in. Fight it with crease geometry and the fight lasts a week. Work with it — by choosing a hinge method suited to the thickness — and it mostly goes away.
The tolerances that matter
Crease-to-cut distance
Where a cut runs close to a crease, the cut edge relieves the crease and the fold becomes weak or the corner tears. There is a minimum practical distance, and it depends on thickness — roughly proportional to it. On a 4 mm sheet, cramming a cut 3 mm from a crease is asking for a ragged fold.
Crease width versus material thickness
A crease that is too narrow sets up a permanent stress concentration and cracks at the fold after a few cycles. Too wide and the fold is floppy and the box is out of square. The rule of thumb is that crease width scales with sheet thickness, and the exact pair should come from the die maker’s experience with the specific sheet — not from a paperboard table.
Flute direction relative to the fold
Folding across the flutes is crisp. Folding along them compresses a long run of flutes and behaves like a hinge with lumps in it. If a design has folds in both directions, one of them will be worse, and the drawing should say which one gets priority.
This is worth deciding at design time rather than discovering at the die trial. On a box with both vertical and horizontal folds, rotating the blank 90 degrees moves the problem from one fold to the other, and usually one orientation is clearly better for the load case.
Why blanks come out off-square
Three contributors, in order of how often they are the cause:
- Die wear. Rules dull unevenly; the middle of a long rule goes first. The blank still separates, so nothing looks wrong until you stack fifty of them and the deviation shows up as a wedge.
- Sheet variation. Thickness and flatness vary across an extruded sheet, and the crease depth that is right at one point is wrong at another.
- Relaxation after cutting. Freshly cut sheet is stressed. Blanks measured straight off the press will measure differently a day later. Let them rest before final inspection, and let them rest before gluing or welding too.
What to put on the drawing
- Sheet thickness and nominal GSM, with the tolerance you will accept
- Flute direction for every fold
- Crease type — compressed flute or partial cut — per fold line
- Flatness acceptance: laid on a flat plate, what gap is acceptable at the corners, measured after 24 hours
That last line is the one that prevents the argument. If flatness is not defined and measured after relaxation, it will be measured at the machine, when the blank is still stressed, and both parties will be right.
When a design fights the material
Some designs have too many folds too close together, or folds that run against the flute direction at acute angles. It can be made to work, but the reject rate at folding will reflect the struggle.
If a design is fighting, the cheapest fix is usually to change the blank layout rather than to chase a better die. Rotating the part on the sheet costs nothing. Specifying a heavier sheet costs a little. Re-cutting a die costs real money — so it is worth sorting out at the drawing stage.
If you send us a blank drawing and the sheet you plan to use, we can flag the fold lines that will give trouble before the die is cut.